

Nickel and zinc plating improve cable-gland surfaces in different ways: nickel provides a barrier and selected wear properties, while zinc can protect compatible iron or steel by being consumed first. I choose between them by the base metal, exposure and job of the coated surface. A gland body, steel locknut and electrical contact can need different coating systems within the same entry.
Process, local thickness, coverage and adhesion determine how the coating works on the finished part. Thread fit, seal lands and mating metals also matter. Start with the actual coating/substrate pair and the required function using the cable-gland material selection guide.
Key takeaways
- Choose a nickel process for the required barrier, wear or contact function; control continuity and adhesion at the working surfaces.
- Zinc on compatible steel provides sacrificial protection, with the coating gradually consumed during exposure.
- Specify local coating thickness at the surfaces that control corrosion and fit, then measure those locations with a suitable method.
- Use salt spray to compare equivalent specimens and service exposure to assess maintenance or life expectations.
- Check wear, thread fit, electrical interfaces and seals on the finished assembly after plating.
Match the surface system to its cable-entry function
A plating system is the base material, pretreatment, deposited layer or layers, thickness class, supplementary finish, post-treatment, and acceptance method considered together. The coating changes the surface that meets the environment and mating parts. The seal compound, cable range, enclosure wall and locknut geometry continue to perform their own mechanical and sealing jobs.
IEC 62444:2010 covers complete-gland construction and performance as supplied. I use coating tests to assess the surface, then check retention, sealing and mechanical functions on the complete gland. The installed entry also includes the cable, wall and mounting parts, so preserve those interfaces when evaluating the finished assembly.
Electroplated nickel and autocatalytic nickel-phosphorus use different processes. Zinc, zinc alloy, passivated zinc, and sealed zinc also form different systems. I identify the actual system from the drawing or coating specification before comparing results.
Nickel performance depends on the deposition system
Electroplated engineering nickel is a functional coating deposited by an electrolytic process. ASTM B689-97(2023) treats hardness, wear, load bearing, corrosion, heat scaling, fretting, and fatigue separately. Fretting is wear associated with small relative movements. The scope also calls for thickness, adhesion, porosity, workmanship, and applicable pre- or post-treatment controls. Those properties guide the deposit type and acceptance checks for the surface being designed.
Nickel often acts as a barrier between the environment and the base metal. A continuous, adherent layer can reduce direct exposure of the substrate. Pores, thin areas, edges, thread damage, or local loss create a different condition. Once an electrolyte reaches the base metal, the coating-substrate pair and exposed-area geometry influence localized attack. Inspect edges and thread-contact areas for damage, and use the specified porosity or continuity test for defects that visual inspection can miss.
Autocatalytic nickel-phosphorus, commonly called electroless nickel, is another coating family. ASTM B733-22(2026) links deposit properties to phosphorus content, heat treatment and bath conditions. Its process can produce uniform thickness on irregular shapes where the solution circulates freely. That makes solution access relevant to threads and recesses; confirm the local minimum at the significant surfaces.
The phosphorus choice also changes the selection. The ASTM scope associates lower-phosphorus deposits with high as-plated hardness and wear resistance, and higher-phosphorus deposits with improved salt-spray and acid resistance in many applications. I choose the composition and heat treatment around the actual wear or chemical duty, then check that finish on the part geometry.
A nickel finish can change hardness, friction and thread behaviour as well as corrosion response. When moving from a flat test panel to a gland body, check the working threads, recesses and wrench flats: their coating distribution and installation damage may differ from the panel.
Zinc protection starts with the substrate
Electrodeposited zinc on steel is a corrosion-protection system in which the coating can be consumed preferentially to protect exposed iron or steel at small local breaks. The active ASTM B633-23 specification is explicitly limited to zinc coatings on iron or steel articles. It defines coating thickness classes, supplementary finishes, preparation, treatment, sampling, and tests. That substrate boundary is decisive for cable-gland selection.
A gland may use a copper alloy while its accessories or enclosure use steel, stainless steel or aluminium. Keep the finish specification attached to each component: B633 applies to the iron or steel part. For a brass body, select a process qualified for that copper alloy. Also assess the galvanic relationship—the electrochemical interaction between contacting metals—in the installed, potentially wet joint.
Passivation and sealers form part of the zinc system and affect exposure behavior. White corrosion products can indicate consumption of zinc; red rust from the steel indicates base-metal corrosion. Distinguish both from dirt or transferred staining, then assess coating loss at the affected location. I use separate acceptance limits for coating corrosion and base-metal corrosion because they mark different stages of protection.
Barrier and sacrificial behavior diverge at a defect
The practical difference becomes clearest at a small discontinuity. An intact nickel system limits access by maintaining a barrier. If a pore or scratch exposes the base metal, the exposed site becomes the critical local interface. A compatible zinc-on-steel system can instead consume zinc around a small break. The cross-sections below show why damage to a barrier and consumption of a sacrificial coating call for different inspection decisions.
Where moisture and geometry support it, zinc consumption can focus around a small exposed steel area. A widening break or depleted coating changes that protection. At a damaged nickel surface, examine the exposed substrate and any undercutting around the defect. At a zinc-coated steel surface, assess both the remaining coating and steel corrosion. In each case, check whether the damage also affects thread engagement or the seal land.
Plating changes five cable-gland interfaces
Plating changes corrosion, wear, dimensions, electrical contact and maintenance needs together. I evaluate each working interface because a useful improvement in one place can create a problem elsewhere. A thicker deposit may help coverage yet consume a fit allowance; a supplementary sealer may change an electrical contact surface.
| Interface | Potential plating effect | Check on the finished assembly |
|---|---|---|
| Exposed body and cap | Changes which metal meets moisture, salts, pollutants, or process chemicals | Compatibility with the actual concentration, temperature, duration, cleaning, and wet-dry cycle |
| Threads and wrench flats | Can change wear, galling tendency, friction, edge coverage, and visible damage | Thread fit, permitted lubricant, tightening method, tool access, and post-installation condition |
| Coated dimensions | Adds material to significant surfaces and may vary across recesses or edges | Drawing dimensions, minimum local thickness, measurement location, and fit after plating |
| Electrical contact path | Changes the contacting surface and its corrosion products | Assigned bonding or screening function, contact pressure, mating metal, fault duty, and test method |
| Seal and enclosure boundary | Can preserve or degrade the metal land that supports adjacent seals | Exact seal, cable, enclosure wall, washer, surface condition, and complete assembly performance |
For a protective or electromagnetic compatibility (EMC) path, I use the bonding and grounding framework. Oxides, passivates, sealers, dirt, contact force, threads and mating finishes control the actual contact. Check resistance and fault-current capacity for the assigned protective function, and assess the specified contact arrangement for screening performance.
Plating changes dimensions as well as the feel of a thread during tightening. Finish, lubricant and the mating surface affect friction. Use the specified assembly torque and check the finished thread against its drawing and gauge requirements. Plan coating allowance before machining so the plated component retains its intended fit.
For a hypothetical smooth cylindrical land, assume a pre-plating diameter of 20.000 mm and a uniform 12 µm coating on every side. Each side adds 0.012 mm, so the finished diameter is 20.024 mm. If the assumed drawing maximum is 20.020 mm, the plated land exceeds it by 0.004 mm. I found that this small coating build-up consumes the fit allowance even though the unplated part meets that assumed limit.
This example uses a uniform layer on a smooth cylinder. A real thread has flank geometry and local coating variation, so set its machining allowance from the thread standard, coating process and finished-part drawing. Check both dimensions and local thickness after plating.
Compare corrosion results under matching exposure conditions
ASTM B117 salt spray testing creates a controlled salt-fog environment for defined specimens. ASTM B117-26a defines the apparatus and exposure conditions; the product specification or test plan supplies the specimen, duration and acceptance rule. Use its results for relative corrosion comparisons under those defined conditions.
To compare two exposure durations, first align the substrates, thickness, pretreatment, added finishes, specimen edges and evaluation criteria. First zinc corrosion and first steel rust are different endpoints. A longer duration to one endpoint may tell you little about a shorter duration to the other. Include replicate specimens and chamber controls so variation is visible.
The ASTM B117 cable-gland guide connects the question, specimen, exposure, and evaluation. I use salt fog to compare controlled systems or check process consistency. Include the gland features that matter to the application, such as working threads, seal lands and edges, in the specimen or supporting evaluation.
For a service-life assessment, connect the corrosion mechanism to field exposure. ASTM B117 calls for corroborating long-term atmospheric exposure when considering correlation or extrapolation. Wetting, drying, dirt, temperature, cleaning, damage, drainage and mixed-metal contact change the service conditions. A coating can delay metal corrosion while seal aging or mechanical damage still determines the entry’s maintenance interval.
A 1936 National Bureau of Standards study of plated steel panels illustrates the difference between appearance and protection. Zinc coatings quickly lost their luster while still protecting steel in rural and marine exposures; acidic industrial atmospheres attacked the coatings more rapidly. Those observations concern the study’s steel panels and historical exposure conditions. For a modern gland, compare the actual finish in the intended environment and track coating loss separately from appearance.
When to consider nickel or zinc
I shortlist the coating by substrate and failure mechanism, then compare its effect on the finished gland. These five steps keep the choice tied to the application:
- Compare the substrate and mating metals: a coating suitable on steel may behave differently on brass.
- Consider salt, chemicals, temperature, wet/dry cycles and abrasion at the joint.
- Identify the needed coating function: barrier protection, sacrificial protection, wear resistance or electrical contact.
- Check coverage at threads, recesses and edges as well as visible flats.
- Compare representative coating data and complete-entry functions separately.
Consider an enclosure entry with a brass gland body and a steel locknut. Specified nickel on the body can serve a barrier or wear function, while a suitable zinc system on the locknut protects its steel sacrificially. They need separate coating specifications. At their shared joint, check wetting, mating surfaces and any assigned electrical path before accepting the combination.
Where recess coverage is the main concern, compare an electroless nickel-phosphorus process with the proposed electroplated deposit and confirm solution access and local thickness. Where steel corrosion at small breaks is the concern, assess the zinc system’s consumption and the extent of exposed steel. Where repeated tool contact is expected, include installation damage and wear in the acceptance checks.
If exposure is unclear, I use the application-environment material guide. It screens temperature, chemicals, weather, mixed-metal contact, and maintenance. If the base metal or seal compound is incompatible with the exposure, change that component first, then select the finish for the revised assembly.
Measure the coating at the surfaces that matter
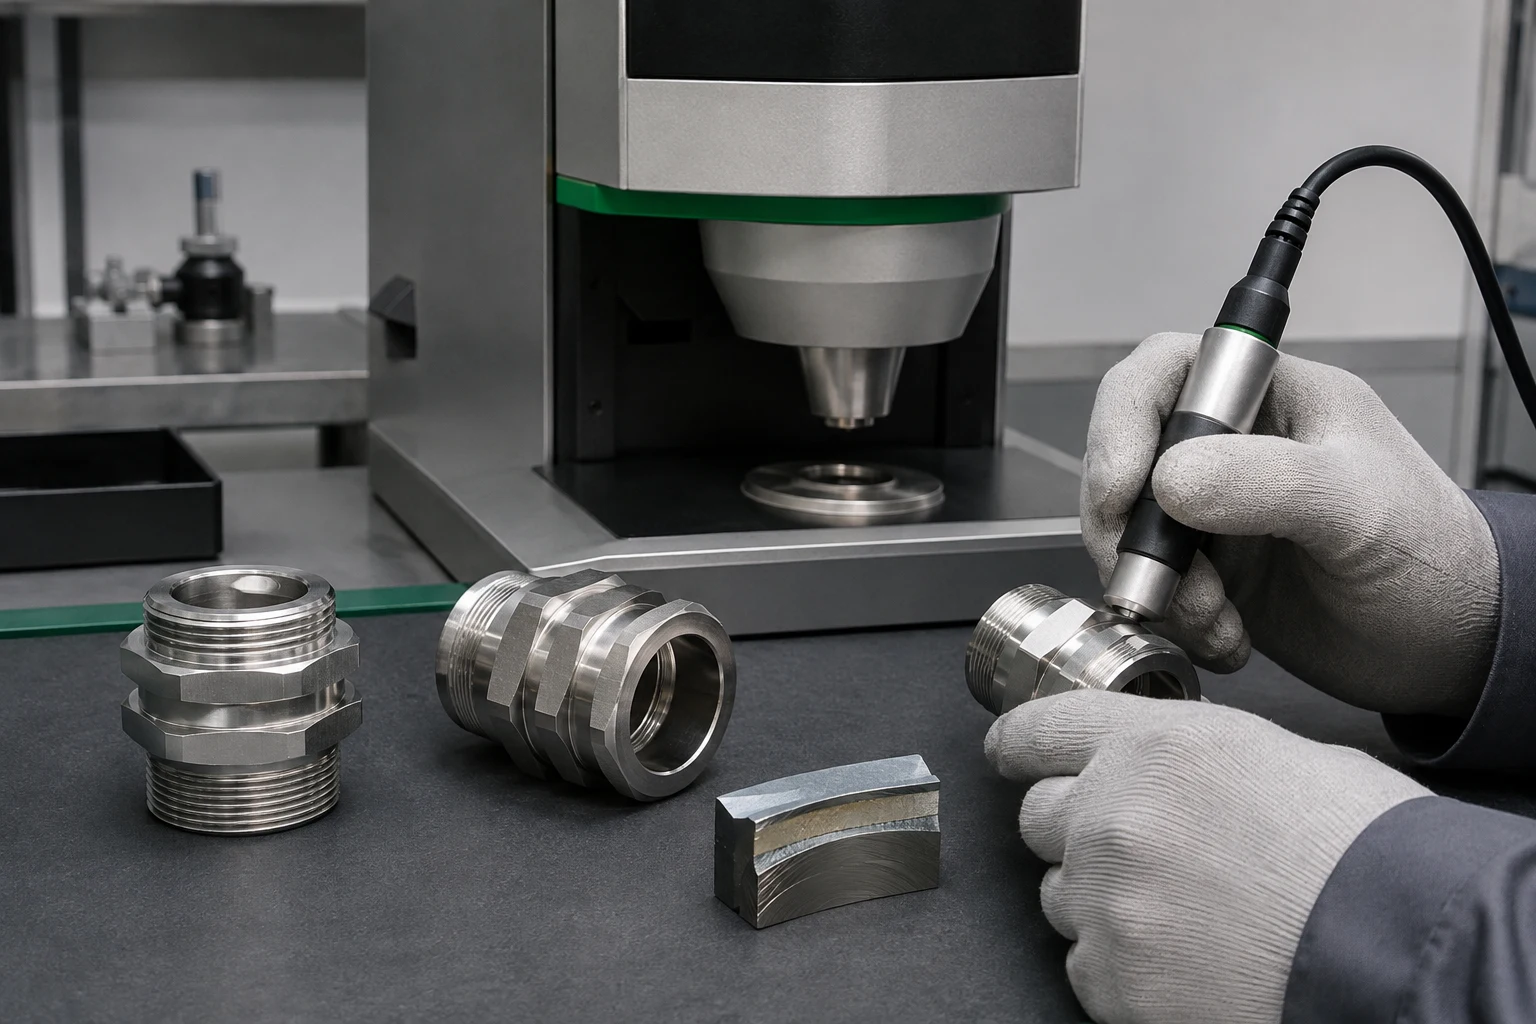
I start with the drawing’s significant surfaces: the locations where coating controls the part’s function. Mark the required measurement positions and minimum thickness, then select a method suitable for the coating/substrate pair. Keep the process and lot identity with the measurements so a thin or damaged area can be traced and corrected.
ASTM B568-98(2021) covers X-ray spectrometry for thickness and sometimes composition. Its range depends on the coating-substrate pair. I check calibration, location, any applicable density assumption, and method capability. Measure accessible flats and use a method suited to the thread roots, edges or recesses identified on the drawing. Check masked areas against their intended boundary.
ASTM B571-23 provides qualitative adhesion tests selected for coating type, thickness, substrate, and end use. If representative panels are permitted, I match base metal and surface finish. The complete preplating, plating, and postplating cycle must also match. That matching preparation and treatment makes the panel relevant to the supplied part.
I separate handling damage from field-corrosion observations. The corrosion diagnosis guide explains discoloration, deposits, pits, blisters, and coating loss. If brass cracking is present, I follow the stress-corrosion investigation. Investigate the crack location, stress and chemical exposure alongside the coating condition.
Conclusion
Nickel and zinc plating extend useful surface performance through different mechanisms. Nickel supplies a barrier and selected wear or contact properties; zinc protects compatible steel through controlled consumption. Choose the process for the substrate and exposure, then control continuity, adhesion and local thickness at the surfaces that matter.
I check the finished threads, seal lands and electrical interfaces before accepting the coated assembly. Use corrosion tests to compare equivalent configurations and field exposure to plan inspection and maintenance. A successful finish preserves the required functions as it ages: it keeps the metal interface serviceable while the seal, cable and mounting arrangement continue to meet their own duties.
FAQs about nickel and zinc plating for cable glands
Is nickel plating always better than zinc plating for cable glands?
Choose by substrate and duty. Nickel can provide a barrier and selected wear properties; zinc can protect compatible steel sacrificially. Match the deposit, local thickness, supplementary finish and exposure to the real part, then check its final fit and working interfaces.
Can ASTM B117 hours be converted into cable-gland service years?
Use B117 hours as a defined laboratory exposure. A service-life estimate requires corroborating field exposure and a supported relationship to the relevant corrosion mechanism. Match wet-dry cycles, temperature, contaminants, damage and mating metals when assessing that relationship.
Can plating color identify whether a gland is nickel or zinc plated?
Identify nickel or zinc through the coating specification and traceable process record, or a suitable analytical method. Color and brightness also vary with preparation, added finishes, sealers, storage and exposure. Use thickness or composition measurements at defined locations when checking the supplied part.
Does nickel or zinc plating prove electrical bonding performance?
Bonding depends on the complete installed path, including contact pressure, oxides or passivates, mating metals, geometry, contamination and current duty. Check the coated assembly using the electrical design and test method for its assigned protective or screening function.
What should a cable-gland plating specification identify?
I identify substrate, coating process and class, composition, local minimum thickness, and significant surfaces. I also specify preparation, underplate, added finish, post-treatment, masking, thread allowance, and repair rule. Tests, sampling, and acceptance criteria need their own detail, together with exposure and cable-entry function.
Sources and technical references
- IEC 62444:2010 - Cable glands for electrical installations, accessed 2026-10-28.
- ASTM B689-97(2023) - Standard Specification for Electroplated Engineering Nickel Coatings, accessed 2026-10-28.
- ASTM B733-22(2026) - Standard Specification for Autocatalytic Nickel-Phosphorus Coatings on Metal, accessed 2026-10-28.
- ASTM B633-23 - Standard Specification for Electrodeposited Coatings of Zinc on Iron and Steel, accessed 2026-10-28.
- ASTM B117-26a - Standard Practice for Operating Salt Spray Fog Apparatus, accessed 2026-10-28.
- ASTM B568-98(2021) - Standard Test Method for Measurement of Coating Thickness by X-Ray Spectrometry, accessed 2026-10-28.
- ASTM B571-23 - Standard Practice for Qualitative Adhesion Testing of Metallic Coatings, accessed 2026-10-28.
- U.S. National Bureau of Standards - Corrosion-protective value of electrodeposited zinc and cadmium coatings on steel, accessed 2026-10-28.