# Cable Gland Thread Geometry: What to Measure Before Gauging
> Source: https://chinacableglands.com/blog/cable-entry-thread-geometry-gauging/
> Language: en
> Publisher: Bepto Cable Glands
> Author: Henry Xu
> Published: 2026-10-22
> Updated: 2026-10-23
## Summary
Read cable-entry thread diameters, calculate metric basic geometry and helix angle, and separate these results from tolerance and gauge acceptance.
## Article
Cable-entry thread geometry starts with three diameters and three different views of the thread. Major, pitch and minor diameters describe its radial form. Pitch and lead describe axial spacing and travel. The profile angle, helix angle and taper angle describe different relationships; substituting one for another gives the wrong answer even when the units look correct.
My starting point is the drawing: mark those quantities, then calculate only the geometry it actually defines. You can use the method below to interpret an entry or discuss a measurement with a supplier. The resulting basic dimensions do not set manufacturing limits, select a drill or approve a mating assembly.
## Locate the three diameters before measuring
On an external thread, the major diameter passes through the crests and the minor diameter through the roots. On an internal thread, the larger major diameter passes through the roots; the smaller minor diameter passes through the inward-facing crests. That reversal matters when someone reports an “inside diameter” without identifying the feature.
The pitch diameter belongs to an imaginary reference surface between them. For an ideal symmetrical thread, thread thickness and intervening space are equal at that surface. The [National Bureau of Standards thread terminology](https://nvlpubs.nist.gov/nistpubs/Legacy/MP/nbsmiscellaneouspub61.pdf), pages 13–14, distinguishes these diameters, pitch, lead and angles. Its geometric definitions apply here; its historical manufacturing limits do not.
External and internal axial half-sections locate the major, pitch and minor reference surfaces relative to the thread axis.
A measured external crest diameter is useful evidence, but it does not reveal pitch diameter. Similarly, measuring the visible mouth of an internal thread can pick up a chamfer instead of a complete crest. Identify the measurement plane and surface before comparing a number with the drawing.
Keep four records distinct: the **basic dimension** is the theoretical reference; the **specified limits** define permitted variation; the **measurement** describes a particular part with uncertainty; and a **plain panel opening** is a separate mounting feature. The [entry-hole sizing guide](/blog/how-to-select-the-correct-entry-hole-size-for-your-cable-gland/) addresses that last task.
## Calculate a metric basic profile
For the ISO metric 60° basic profile, let nominal major diameter be $d=D$ and axial pitch be $P$, all in millimetres. The fundamental sharp triangle has height $H$. Its truncations give the basic pitch diameters $d_2$ and $D_2$, and basic internal minor diameter $D_1$:
$$
H=\frac{\sqrt{3}}{2}P,\qquad d_2=D_2=d-\frac{3}{4}H,\qquad D_1=d-\frac{5}{4}H
$$
The metric profile in [Union College’s machine-design notes](https://rbb.union.edu/courses/mer419/content/data/Lectures/MER419%20L09%20Fastener%20Stiffness.pdf), slide 9, shows the 60° triangle and its radial subdivisions. Doubling the relevant radial offsets gives the diameter reductions above. Production values need the governing drawing and controlled standard.
For our worked example, a nominal 20 mm diameter and 1.5 mm pitch give:
| Quantity | Calculated basic value | Meaning |
| --- | ---: | --- |
| Fundamental triangle height | 1.299038 mm | Height before the profile truncations |
| Pitch diameter | 19.025721 mm | Basic reference diameter between crests and roots |
| Internal minor diameter | 18.376202 mm | Basic diameter through the internal crests |
| Radial basic engagement height | 0.811899 mm | Five eighths of the fundamental triangle height |
The extra digits let us reproduce the arithmetic; they are not a measurement capability or an inspection tolerance. In particular, **18.376202 mm is not the manufactured external root diameter**. External root design, radius, tolerance, coating and the applicable limits require their own specification.
### [Metric basic thread diameters](https://chinacableglands.com/resource-center/tools/metric-basic-thread-diameter-calculator/)
Category: Threads & entry geometry
Calculate ISO metric 60° basic-profile pitch diameter, internal minor diameter and fundamental triangle height from nominal major diameter and pitch.
Formula: ` H = √3P/2; d₂ = D₂ = d − 3H/4; D₁ = d − 5H/4 `
Inputs:
- Nominal basic major diameter
- Axial thread pitch
Article note: Enter the specified metric 60-degree nominal diameter and pitch. Read D1 as the basic internal minor diameter; apply actual tolerance, external-root and gauging requirements separately.
For the same reason, the calculated internal minor diameter is not a drill instruction. The machining process needs its permitted finished dimensions, material, tool and method. Basic geometry supplies a reference, not the whole process.
## Separate profile angle, helix angle and taper angle
The included profile angle is viewed in an axial section. For the metric basic form above it is 60°, with each symmetrical flank at 30° to a line perpendicular to the thread axis. The helix angle describes how a thread winds around a reference cylinder. A taper angle describes how the reference diameter changes along the axis.
Every quoted angle needs its reference line. An angle measured to the axis is complementary to one measured to a plane perpendicular to it, so an unexplained “thread angle” can produce a large apparent disagreement.
Pitch is the axial spacing between adjacent corresponding profiles. Lead $L$ is the advance of one helix in a complete turn. For $n$ starts:
$$
L=nP,\qquad \lambda=\tan^{-1}\left(\frac{L}{\pi D_m}\right)
$$
Here $D_m$ is the stated mean or pitch diameter, in the same unit as $L$, and $\lambda$ is the angle to the plane perpendicular to the axis. Unrolling the reference cylinder gives a right triangle: circumference is the horizontal length and lead is the rise. This geometric construction is the basis of the equation.
Using the example's basic pitch diameter, a single start gives a lead of 1.5 mm and an angle of about 1.438°. An assumed two-start geometry with the same pitch and reference diameter would have a 3.0 mm lead and about 2.873°. The second result is a comparison, not a claim that a standard M20 cable-entry part has two starts. Use the actual drawing to establish the start count.
## Read taper, roots and incomplete thread regions
For a stated diameter change $\Delta D$ over axial distance $\ell$, diameter taper is $\Delta D/\ell$. The corresponding cone half-angle is $\tan^{-1}(\Delta D/(2\ell))$. The factor of two appears because the cone angle follows the change in radius, not diameter.
As a geometric example, a 0.50 mm diameter change over 8.0 mm gives a 1:16 diameter taper and a half-angle of about 1.790°. This does not identify the thread family. Profile, pitch, reference plane, limits and gauging still distinguish the actual interface.
A **root** is the valley between adjacent thread flanks. **Runout** is the transition where complete thread form ends. An **undercut** is an intentionally relieved region, often providing tool or mating-part clearance. Mark the last complete profile and shoulder separately: the distance to the end of the component can exceed its usable full-form thread length.
For an entry that stops before the shoulder seats, that distinction is practical. Compare the male runout, female depth, chamfer and shoulder clearance before concluding that the diameter is wrong. The [M20 pitch guide](/blog/m20x1-5-vs-m20-the-engineers-guide-to-fine-pitch-gland-threads/) covers the different symptom caused by conflicting pitches.
## Choose the measurement that answers the question
The feature and acceptance rule determine the instrument; different “thread checks” answer different questions.
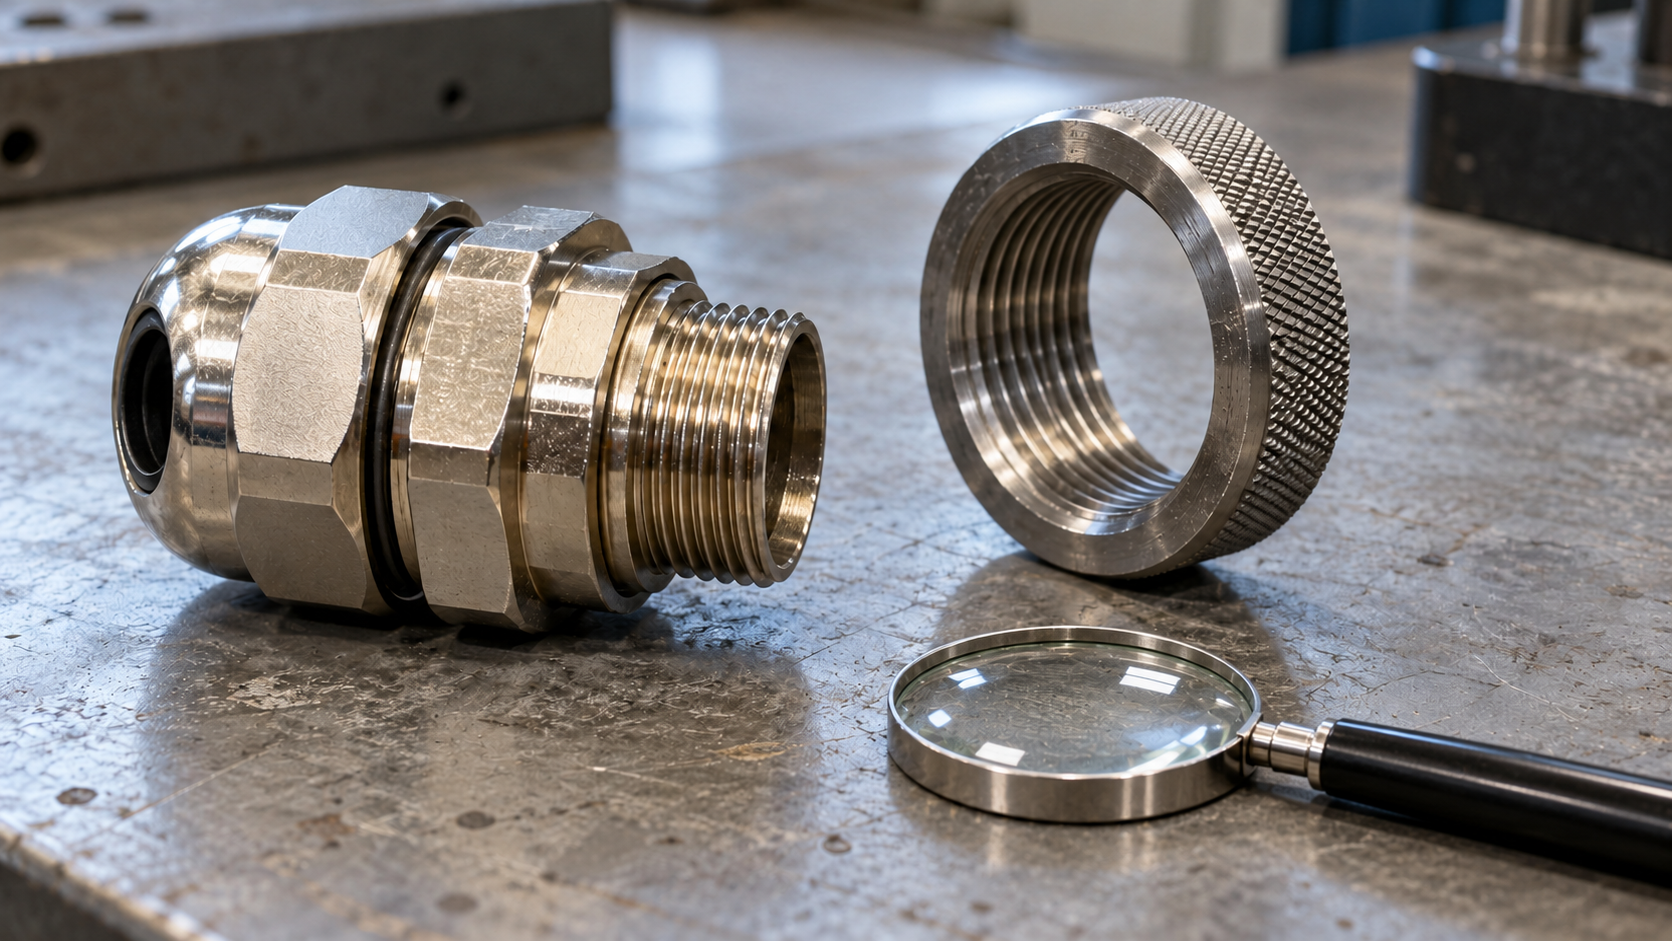
The exposed entry thread and threaded ring sit beside a magnifying glass for surface inspection.
| Method | Useful question | Remaining limitation |
| --- | --- | --- |
| Caliper | Is accessible crest diameter consistent with a candidate size? | Does not establish the full functional thread form |
| Pitch leaf | Does spacing resemble the stated pitch? | Does not establish tolerance class or lead accuracy |
| Thread plug gauge | Does the internal thread satisfy the specified gauging criterion? | Requires the correct standard, size, class and procedure |
| Thread ring gauge | Does the external thread satisfy its gauging criterion? | Requires the corresponding external-thread acceptance basis |
| Profile or coordinate measurement | What are the defined individual geometry results? | Requires suitable probing, alignment and uncertainty evaluation |
[ISO 1502:1996](https://knowledge.bsigroup.com/products/iso-general-purpose-metric-screw-threads-gauges-and-gauging) addresses gauges and gauging for general-purpose metric screw threads. [ISO 965-1:2026](https://knowledge.bsigroup.com/products/iso-general-purpose-metric-screw-threads-tolerances-principles-and-basic-data-3) addresses their tolerance system. These are different tasks from calculating a basic profile. NIST's [pitch-diameter measurement paper](https://www.nist.gov/publications/pitch-diameter-measurement-threaded-gages-using-cmm) also identifies the complexity and uncertainty of CMM thread measurement.
A reproducible result needs a record of the drawing revision, gauge identity and calibration status, finished or unfinished part state, cleaning, relevant temperature conditions and the applied acceptance procedure. Do not import a universal number of permitted NO-GO turns into a thread family that uses a different rule.
## Conclusion: Keep geometry attached to its reference
Locating the major, pitch and minor surfaces gives us a starting point for interpreting a cable-entry thread; axial pitch and lead then stay separate from profile, helix and taper angles. The metric example shows how a nominal diameter and pitch generate basic reference values, including an internal minor diameter that must keep its correct name.
Before using those values to judge a part, return to the drawing's limits and measurement method. Check the actual root, complete thread length, runout and shoulder as well as diameter. This makes the calculation useful for communication while leaving fit, sealing and assembly acceptance with their specified evidence.
## FAQ
### Is pitch diameter the average of major and minor diameters?
Not generally. It is defined by the thread's reference geometry, rather than by averaging any two measured diameters. Crest truncation, root form and tolerances matter. I use the specified pitch diameter or a justified reference diameter when calculating helix angle, and record exactly which value was entered.
### Does the metric calculator return the external root diameter?
No. Its minor-diameter output is the basic internal minor diameter D1. A manufactured external root has its own profile and dimensional limits. I keep those quantities separate when comparing a calculated result with a drawing or measurement, even when an older reference diagram shares basic-profile labels.
### Why can equal-pitch threads have different lead angles?
A multiple-start thread advances by the pitch multiplied by the number of starts in one turn. The reference diameter also changes the circumference of that turn. Both lead and diameter therefore affect the angle. The start count and reference surface must accompany the result.
### Can a matching pitch leaf replace a thread plug or ring gauge?
No. A pitch leaf helps identify spacing. The applicable plug or ring gauge evaluates a different acceptance condition for a specified thread. I use the correct gauge and procedure when conformity is required, including the specified part condition and current calibration record.
### Sources and technical references
- [Union College — MER419 Machine Design, Joint Fasteners, metric profile slide 9](https://rbb.union.edu/courses/mer419/content/data/Lectures/MER419%20L09%20Fastener%20Stiffness.pdf), accessed 2026-10-22.
- [National Bureau of Standards — Report of the National Screw Thread Commission, terminology pages 13–14](https://nvlpubs.nist.gov/nistpubs/Legacy/MP/nbsmiscellaneouspub61.pdf), accessed 2026-10-22.
- [ISO 1502:1996 — ISO general-purpose metric screw threads, gauges and gauging](https://knowledge.bsigroup.com/products/iso-general-purpose-metric-screw-threads-gauges-and-gauging), accessed 2026-10-22.
- [ISO 965-1:2026 — ISO general purpose metric screw threads, tolerance principles](https://knowledge.bsigroup.com/products/iso-general-purpose-metric-screw-threads-tolerances-principles-and-basic-data-3), accessed 2026-10-22.
- [NIST — Pitch Diameter Measurement of Threaded Gages Using a CMM](https://www.nist.gov/publications/pitch-diameter-measurement-threaded-gages-using-cmm), accessed 2026-10-22.